Industrial Ethanol – High-Purity, High-Quality, Reliable Chemical Product
Product Overview
Industrial Ethanol is a versatile chemical product which is commonly used as a solvent, processing agent, extraction medium, and a raw material in a wide range of industries. With excellent solvency, fast evaporation, and compatibility with a wide range of substances, ethanol is used as a critical component in chemical manufacturing, pharmaceuticals, cosmetics, personal-care products, cleaning products, laboratory settings, and many other applications.
Our ethanol is supplied with the focus on quality, performance, appropriate packaging, and reliable bulk availability, making it a viable choice for manufacturers, distributors, importers, wholesalers, and others.
Key Features of Industrial Ethanol
High-Quality & Reliable Performance
Our ethanol is handled and supplied to ensure consistent characteristics across batches and deliveries. Customers may choose from a range of ethanol grades and specifications according to their area of application.
Excellent Solvent Properties
Ethanol is capable of dissolving a wide range of organic and inorganic substances, making it a versatile solvent in the fields of chemical manufacturing, industrial processing, and other solvent-dependent applications.
Fast Evaporation
This product is a highly volatile chemical solvent with one of the faster evaporation rates in its class. Ethanol’s strong evaporation properties make it particularly valuable in situations which require fast removal after use.
Highly Versatile Chemical
From manufacturing and formulation to cleaning and extraction, ethanol can fulfill multiple roles as a critical component or a processing medium in a wide range of commercial and industrial applications.
Major Industrial Applications
1. Chemical Manufacturing
Ethanol is a common component in the chemical industry where it is used as a solvent, processing agent, and a material in a wide range of chemical formulations and products.
2. Pharmaceutical Applications
Depending on the grade and regulatory standards, ethanol can be used in the pharmaceutical industry, including laboratories, manufacturing, extraction, formulation, and other technical applications.
3. Cosmetics & Personal Care
Ethanol is a critical component in many cosmetic and personal-care formulations, including perfumes, sprays, lotions, and similar products.
4. Fragrance & Perfume Industry
Due to its strong solvent properties and evaporation characteristics, ethanol is commonly used in the perfume and fragrance industry as a solvent, carrier, and a processing medium.
5. Industrial Cleaning
Ethanol’s solvent properties are often utilized in numerous industrial applications, such as surface cleaning and treatment, through specially-designed solutions.
6. Laboratory & Research Applications
In laboratories, ethanol may be used in various applications including cleaning, extraction, processing, and other relevant operations.
7. Manufacturing & Processing
Industrial manufacturers can utilize ethanol in various applications where a solvent or processing medium is required. The required grade and specifications must be chosen according to the intended use.
Packaging & Bulk Supply
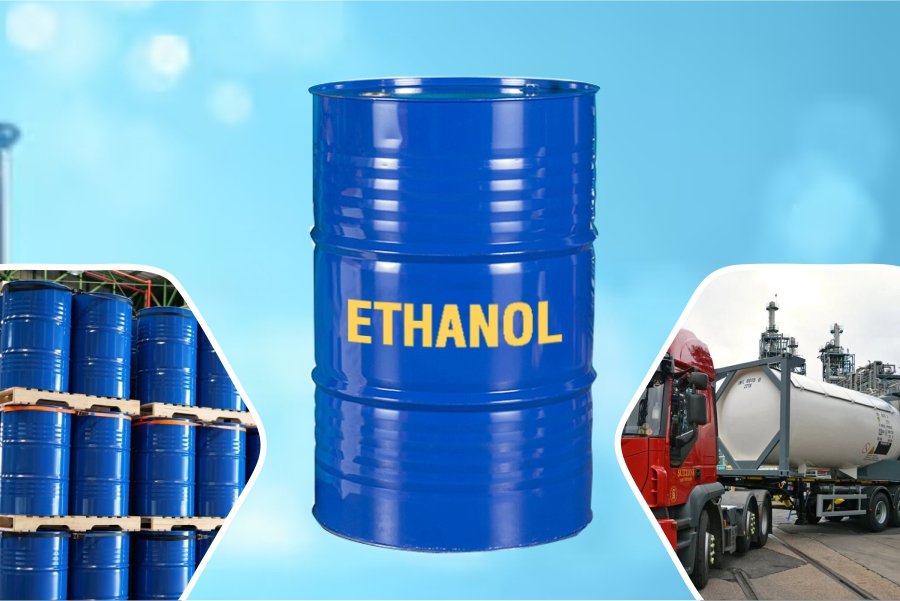
Our Industrial Ethanol can be supplied to meet customer requirements, including:
- Industrial drums
- Bulk supply
- Tanker shipments
Customized commercial supply arrangements
The packaging and transportation methods will be determined according to the quantity, destination, regulatory requirements, and customer specifications.
Quality & Supply Reliability
For industrial buyers, the consistency and reliability of supply are often as important as the properties of the material itself. We focus on providing:
Consistent Specifications
Ethanol can be supplied according to customer specifications, including quality and technical requirements.
Flexible Quantities
We offer flexible supply options for distributors and manufacturers who require bulk supplies on a regular basis.
Professional Handling
Due to ethanol’s flammable nature, it is necessary to handle it with care. We follow all relevant safety standards to ensure the safety of our customers as well as our operations.
International Supply
The product can be considered for international commercial supply, subject to applicable export, import, hazardous-material, and destination-country regulations.
Why Choose Our Industrial Ethanol?
✔️ High-quality product
✔️ Consistent performance
✔️ Multiple industrial applications
✔️ Bulk supply capability
✔️ Flexible packaging options
✔️ Suitable for manufacturers and distributors
✔️ Professional logistics support
✔️ International sourcing and supply opportunities
Ideal for Global Industrial Buyers
Our Industrial Ethanol is an excellent choice for industrial buyers who are looking for a versatile, reliable, and commercially viable chemical product for their manufacturing and formulation needs. The product’s wide range of applications makes it especially valuable for businesses in the chemical, pharmaceutical, cosmetic, fragrance, cleaning-products, laboratory, and general manufacturing industries.
Whether you are in need of regular ethanol supply, bulk distribution, or international sourcing, we are here to help you find a reliable supply solution which fits your technical and commercial requirements.
Get in Touch for Bulk Ethanol Supply
Looking for a reliable supplier or export partner for Industrial Ethanol? Contact us to learn more about the product specifications, commercial terms, and requirements for your industry or country. Our team can provide the relevant information about the specifications and commercial aspects of your ethanol supply.